news center
recommending products
contact: mr. jin
tel: 13901575780
0512-52428686
contact: mr. zha
tel: 13913639797
0512-52422071
address: no. 59, huyi road, liantang, shanghu town, changshu city, jiangsu province.
what should be noted during the daily maintenance of tungsten steel pipe cutting saw blades
the tungsten steel pipe cutting saw blade has high hardness but weak impact resistance. the blade edge is precise, and daily maintenance revolves around cleaning, inspection, cooling, grinding, storage, disassembly and protection to reduce problems such as tooth breakage, substrate deformation, and premature wear.sources:k8凯发旗舰 | publishdate:2026.10.08
1、 cleaning treatment after each assignment
after each cutting operation, promptly clean the metal chips, cutting oil, and chip deposits attached to the saw teeth and saw blade substrate. soft brush and dust-free cotton cloth can be used for cleaning, without using hard steel shovel or wire brush to scrape the blade edge, to prevent scratching the tungsten steel blade head and the surface of the saw blade substrate.
after cleaning, completely dry the saw blade and remove any residual cutting fluid. under humid conditions, a thin layer of anti rust oil can be applied to the saw blade substrate and teeth to prevent long-term storage from causing rust. rust spots can disrupt the dynamic balance of the saw blade and increase cutting vibration. during cleaning, check the inner hole and flange fitting surface synchronously, remove oil and impurities, and avoid deviation after assembly.
2、 appearance and working condition inspection before and after homework
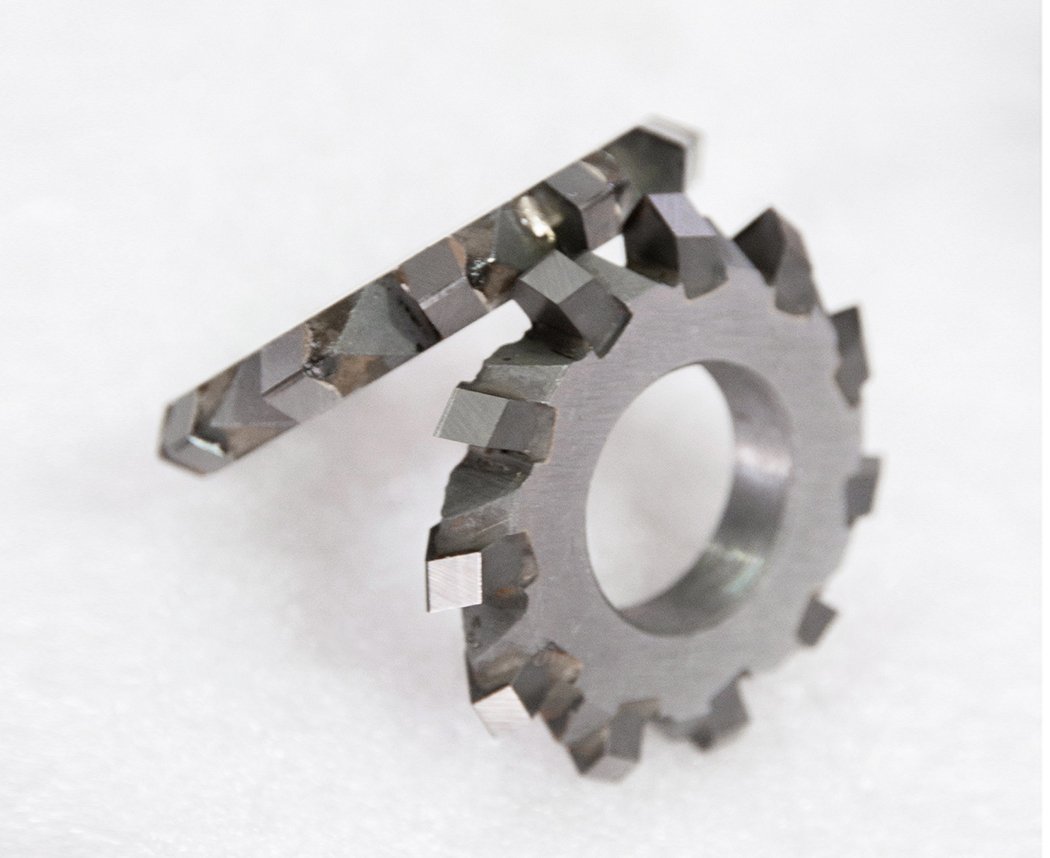
before starting up, visually inspect the condition of the saw blade, check for any dents, cracks, or missing teeth in the tungsten steel teeth, check for any distortion or deformation in the base material, and check for any cracks in the weld seam position. do not put defective saw blades into cutting operations to prevent safety risks during use.
check the main shaft and flange of the equipment, ensure that the flange contact surface is flat and clean, and that the specifications of the two flanges are consistent. after installation, confirm that the saw blade has no obvious jumping. after assembly, the new saw blade or the polished saw blade should be idle for a period of time to confirm smooth operation before cutting the pipe.
pay attention to equipment vibration, noise changes, and pipe cutting status during the cutting process. if there is a significant increase in burrs on the incision, an increase in cutting resistance, and intensified abnormal noise, the machine should be stopped for inspection and cutting should not continue with the fault. at the same time, observe the cooling and lubrication system to confirm that the nozzle is unobstructed and the cutting fluid can continuously cover the cutting area.
3、 cutting cooling and parameter control
choose suitable cutting fluid or trace lubricating medium according to the material of the pipe, and try to avoid long-term dry cutting. continuous cooling can remove the heat generated by cutting, prevent high-temperature annealing of tungsten steel cutting heads, reduce the hardness of cutting heads, and accelerate wear.
control the feed rate and spindle speed reasonably to avoid feed impact and forced downward pressure on the pipe material. tungsten steel cutting heads are not resistant to instantaneous impact, and unstable clamping of pipes and excessive feed can easily cause tooth breakage. when cutting thin-walled pipes, reduce the feed rate, decrease the tooth load, and minimize tooth damage caused by vibration.
4、 saw blade grinding management
when the quality of the incision deteriorates, the load significantly increases, or the cutting edge shows normal wear, promptly send it to a professional organization for grinding. do not wait until the tooth head is severely damaged before processing. grinding requires retaining the original tooth profile, front angle, and back angle parameters of the saw blade, and cannot arbitrarily change the geometric angle of the tooth part, while ensuring that the dynamic balance meets the standard after grinding.
reasonable control of single grinding amount to avoid excessive grinding causing tool head loss. if the tungsten steel teeth are extensively damaged and cracks appear in the substrate, it is generally not recommended to repair them, and a new saw blade can be evaluated for replacement.
5、 dismantling and storage protection
when disassembling and transporting saw blades, wear protective gloves to avoid bumping or hitting the serrated areas, and do not touch sharp edges with bare hands.
saw blades that are not currently in use should be stored vertically first; if stored flat, do not stack heavy objects above the saw blade to prevent deformation of the substrate under pressure. the storage environment should be kept dry and ventilated, away from corrosive gases and humid areas. different specifications of saw blades should be stored separately to avoid collision between tooth heads. complete cleaning, drying, and rust prevention treatment before long-term storage.